Understanding 2307m: Industry Context and Practical Guidance
This guide explains what 2307m typically refers to in industrial measurement or component labeling and how to evaluate suppliers, specs, and compliance factors with a disciplined, objective approach. Background information is provided on how such identifiers are used across technical supply chains, what due diligence should cover, and which verification steps reduce mismatch risk when ordering from different vendors.
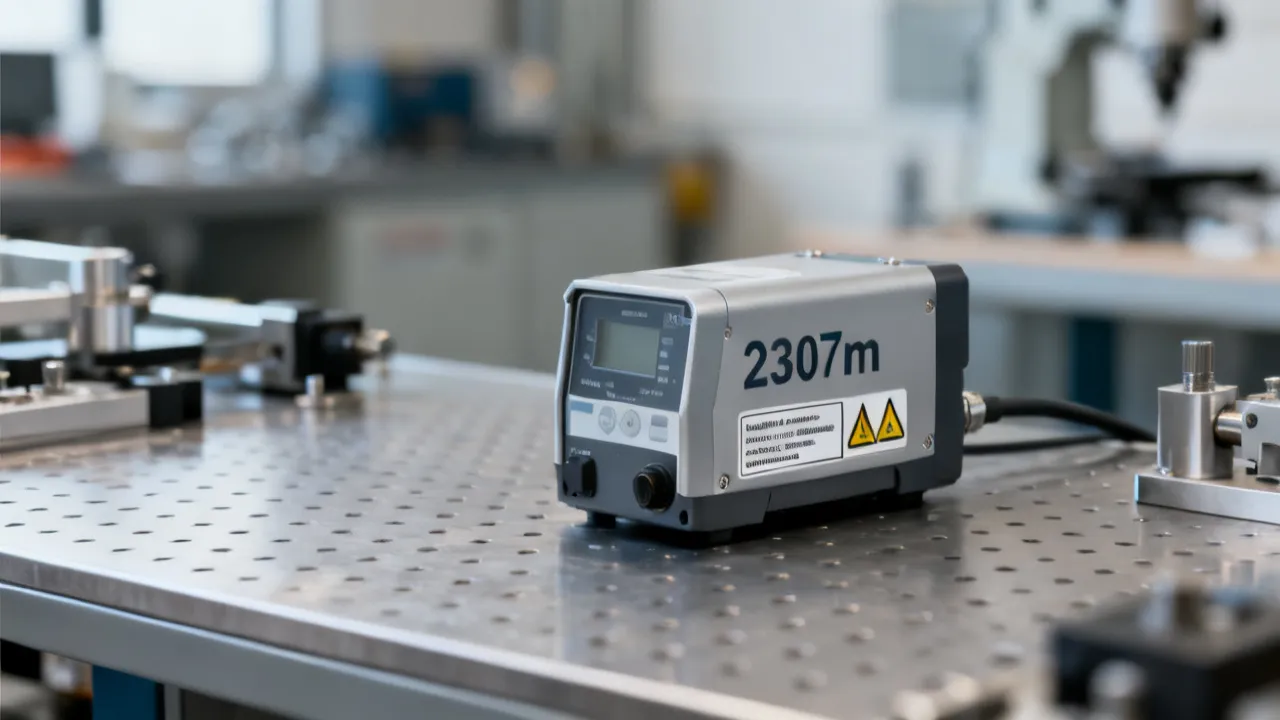
1) Why “2307m” Matters: Define It Precisely Before You Buy
When you encounter the identifier 2307m in a technical context, treat it as a starting point—not a final specification. In many industrial settings, labels like 2307m may correspond to a part number, a calibration reference, a measurement range, a model variant, or a packaging/lot reference. The practical implication is straightforward: if the identifier is not mapped to the exact technical documentation (drawings, tolerances, test reports, or a datasheet), you risk ordering the wrong component even if the label appears to match.
From an industry-expert perspective, the most reliable evaluation method is to confirm the identifier against authoritative materials provided by the supplier or through verifiable standards documentation. This is especially important when procurement spans multiple vendors or regions, where naming conventions can vary even when the physical item is intended to be the same.
It can help to think of 2307m the way you would think of a library call number: the identifier alone is not the book’s content; it is merely a pointer into a specific catalog entry. If the pointer is wrong, outdated, or points to a different edition (revision), your “purchase” might contain the right-looking cover but the wrong internal chapters.
Additionally, 2307m can be easy to misinterpret because it resembles a compressed code that might include multiple embedded meanings (for example, “230” might indicate a family, while “7m” indicates a variant, manufacturer, or measurement condition). Without clarification in controlled documentation, two suppliers can produce parts that are visually similar, physically compatible in a loose sense, but different in ways that matter—such as material grade, surface finish, environmental rating, calibration method, or dimensional tolerance class.
Therefore, the first procurement principle is: do not buy the label; buy the documented characteristics tied to the label. The identifier is simply the trailhead. Your due diligence is to verify that the documentation trail is real, current, and aligned with your intended use.
2) Objective Background: How Technical Identifiers Are Used
Identifiers such as 2307m are common in industrial ecosystems because they allow manufacturers and suppliers to coordinate production, inventory, and documentation. In principle, these identifiers act as anchors that connect the physical item to:
- Technical specifications (dimensions, material grade, performance limits)
- Verification artifacts (inspection reports, batch traceability records, compliance statements)
- Compatibility claims (fit/form/function alignment with interfaces or assemblies)
However, the “meaning” of an identifier is not always identical across companies. Two different vendors may use similar-looking labels to refer to different variants unless the procurement documents clearly specify the governing standard, revision level, and measurable acceptance criteria.
To understand why mismatch happens, it helps to map the lifecycle of an identifier. Many part numbers or codes start as internal manufacturing references. Over time, those references become external-facing IDs used for purchasing. If a vendor changes:
- process steps (e.g., a new heat treatment method),
- supplier inputs (e.g., a different alloy or polymer batch),
- measurement technique (e.g., updated calibration tools),
- tolerance band (tighter or looser acceptance), or
- design revision (a change that affects interface geometry),
…then the identifier may be maintained while the underlying technical meaning changes—or it may be updated in documentation but not reflected consistently on the packaging or paperwork. This is why revision control is not an administrative detail; it is a technical risk control.
In mature quality systems, these changes are managed through controlled engineering change orders, documented revision histories, and consistent labeling. But in less mature systems, identifiers can drift relative to their documented characteristics, especially when multiple subcontractors are involved.
Therefore, objective background means recognizing that identifiers are intended to be stable keys in a database of truth. Your job in procurement is to confirm that the key actually resolves to the correct database record for the specific revision and acceptance criteria relevant to your application.
3) What You Should Verify for “2307m” (Key Procurement Questions)
To evaluate any offer that references 2307m, focus on verification questions that can be answered with evidence rather than marketing language:
3.1 Documentation and revision control
Request the supplier’s datasheet or technical drawing that explicitly references 2307m, including revision number and effective dates. If the supplier provides only photos or informal descriptions, treat that as a gap in traceability.
When requesting documentation, do not stop at “latest datasheet.” Ask for the controlled document number and revision, and confirm that your quote line item is tied to that exact revision. If the supplier uses terms like “current version” or “equivalent,” ask them to specify what is equivalent and to which revision it is being compared.
Also ask how the supplier handles “cross-references.” Some companies offer substitutions that they claim are functionally equivalent. If they do, insist on documented equivalence criteria (dimensional differences, material substitutions, performance deltas, and test results). Without that, you may be accepting a substitution that affects your installation, reliability, or compliance requirements.
3.2 Performance and acceptance criteria
Identify what success looks like in measurable terms. For example, the offer should state tolerances, test methods, and allowable deviations. If 2307m is associated with a measurement capability or specification level, you should confirm the test protocol used to establish it.
In many industrial disputes, the disagreement is not whether the supplier “met the spec,” but rather whether the spec being used is the same spec documented in procurement. This is why you should request:
- Acceptance criteria (what values are acceptable and under what conditions)
- Test method (standards or internal test procedure identifiers)
- Test conditions (temperature, pressure, load profile, timing, sampling plan)
- Measurement uncertainty (especially for calibrated or metrology-related items)
Even seemingly minor phrasing matters: “meets specification” is not the same as “tested per Method X, acceptance limit Y, results recorded in batch record.”
3.3 Traceability and lot/batch records
Ask whether the product includes batch/lot traceability (serial number ranges, manufacturing date codes, or production batch IDs). This becomes crucial for audits and troubleshooting.
Traceability typically has at least two dimensions:
- Identity traceability: can you confirm what was shipped and to which manufacturing batch it belongs?
- Evidence traceability: can you connect that manufacturing batch to inspection/test records, certificates, or conformance evidence?
If you operate in regulated environments (aerospace, medical device, automotive safety, energy, or pharmaceuticals), evidence traceability is often required. Even outside heavy regulation, good traceability shortens root-cause analysis time when failures occur.
If the supplier cannot provide lot information—or only provides it in a form that is difficult to map to shipping paperwork—then you may still receive product, but you will have degraded your ability to verify compliance and manage risk.
3.4 Compatibility and interface requirements
If your application depends on fit, sealing, mounting, electrical/thermal characteristics, or environmental ratings, request interface specifications—such as mounting patterns, connector types, or environmental limits—and confirm compatibility with your system’s requirements.
Compatibility is a multi-layer concept. It includes:
- Mechanical interfaces (dimensions, thread standards, gasket/seat geometry, tolerances)
- Electrical interfaces (pinout, insulation class, impedance, contact resistance)
- Thermal interfaces (operating temperature range, thermal conductivity, heat dissipation characteristics)
- Environmental interfaces (humidity, corrosion resistance, ingress protection, chemical compatibility)
- Functional interfaces (response time, calibration stability, throughput, signal characteristics)
When 2307m is only a partial identifier, compatibility risk can increase if the supplier expects you to “know” the intended interface standard. For procurement safety, require the supplier to confirm the interface details and provide documentation that supports that confirmation.
4) Supplier Evaluation: Evidence-Based Criteria
Procurement decisions often fail not because the price is wrong, but because the evidence trail is incomplete. For items labeled 2307m, use an evaluation checklist that emphasizes verifiable documentation:
- Quality management system: Evidence of recognized quality frameworks (e.g., documented process controls).
- Inspection and test capability: Reference to testing methods used to verify specs.
- Correctness of labeling: Clear linkage between the physical item and 2307m in shipped documentation.
- Responsiveness to RFQ details: Whether the supplier can answer spec questions with specific documents.
In objective terms, the best suppliers do not rely on “trust us” claims; they provide materials that a technical team can review and compare to internal requirements.
However, supplier evaluation should also include a “behavioral” dimension: how the supplier responds when you ask for controlled documents, revision numbers, or acceptance evidence. This is not about politeness; it’s about operational maturity.
For example:
- If a supplier can quickly provide a controlled datasheet and revision—without ambiguity—that suggests their internal traceability is strong.
- If a supplier delays, says the documentation is “not available,” or provides a generic brochure, that suggests their product might not be controlled to the level you need.
- If they provide conflicting revision numbers between quote documents and shipped paperwork, that suggests they cannot maintain a reliable linkage between the identifier and the evidence chain.
To refine supplier evaluation, consider requiring a “procurement packet” (sometimes called a submittal package). This typically includes:
- Controlled drawing or datasheet for 2307m (with revision)
- Certificate of conformance / inspection report
- Batch/lot traceability evidence
- Any calibration certificate or test report (if applicable)
- Packaging/labeling specification confirmation (if you need specific marking)
When suppliers know that you will validate those items, they are more likely to deliver consistent documentation rather than “minimum compliance.”
5) Price Considerations Without Overstating: What Impacts Cost for “2307m”
You mentioned price information and supplier details, but the specific numeric price and supplier identity were not provided in the prompt. In the absence of a confirmed price, the most responsible guidance is to explain what typically drives cost variation for components or measurement-related items such as 2307m.
Common cost drivers include:
- Material grade and processing: Better-grade materials or tighter tolerances generally increase cost.
- Testing and documentation: Items that include more extensive test reports and traceability records may cost more.
- Revision matching: A “near match” to 2307m can be cheaper, but riskier.
- Lead time and logistics: Expedited shipping, packaging requirements, and customs handling can affect the final invoice.
For stakeholders comparing quotes, the professional approach is to normalize the comparison: compare like-for-like revisions, documentation packages, and acceptance criteria, not only unit price.
It is also useful to consider total cost of ownership (TCO). A low unit price can become high cost if it triggers rework, field failures, warranty claims, downtime, or compliance gaps. Procurement teams often overlook TCO because it sits across functions—quality, engineering, operations, maintenance—but it is usually where the real cost of mismatch lives.
To manage TCO, ask questions such as:
- Will the documentation packet be accepted by internal quality review?
- Is incoming inspection likely to pass without discrepancy?
- If a discrepancy is found, can the supplier respond with corrective action evidence (not just “replacement”)?
- Does the item require calibration or special handling that adds downstream costs?
Additionally, price can vary due to sample testing or certification scopes. For example, one supplier may provide a certificate of conformance based on production records, while another may provide a full inspection report or sample test data. If your application requires the latter evidence, the more expensive quote may actually be the cheaper option when considering risk and verification labor.
When you normalize quotes, you are essentially converting “price” into “price for a defined evidence package.” That conversion makes procurement decisions fair and defensible.
6) Quality and Compliance: How to Reduce Mismatch Risk
Even when 2307m appears identical on paper, mismatch risk can arise from:
- Revision drift: The part number may remain the same while internal revisions change tolerances or materials.
- Interpretation gaps: A vendor may interpret “2307m” according to their catalog rather than your application’s requirements.
- Documentation inconsistency: Shipping paperwork may not match the actual test/inspection artifacts.
To reduce these risks, insist on a procurement packet that includes specification documents and test/inspection statements where applicable.
Mismatch risk also increases when:
- The item is sourced through distributors rather than direct manufacturers (risk of relabeling or outdated stock)
- The supplier is using alternative materials for cost reasons without engineering change authorization
- Lead time pressure causes suppliers to substitute “available” parts while maintaining the same identifier
- Receiving inspection is limited to quantity count rather than identity and evidence checks
One practical mitigation is to define acceptance gates. Instead of waiting until the product fails in operation, you define points where product must prove itself:
- Gate 1 (Pre-shipment): confirm documentation revision alignment and evidence packet completeness.
- Gate 2 (Upon receipt): verify identity and basic physical marking match 2307m.
- Gate 3 (Functional/engineering validation): run tests relevant to your application to confirm performance characteristics.
- Gate 4 (In-service monitoring): maintain feedback loops for continuous improvement and supplier quality tracking.
In mature organizations, supplier performance is measured and feedback is structured. If 2307m items fail or documentation mismatches occur, the supplier’s quality rating can degrade, which incentivizes better evidence and revision control.
7) Localized Procurement Mindset: “nearby” Considerations
Your prompt contains no explicit city or country; however, it references localization rules and includes the placeholder concept of “nearby.” In practice, when sourcing “nearby,” procurement teams often balance lead time, communication speed, and return logistics with the broader question of documentation quality. For example, many organizations prefer suppliers “nearby” when rapid clarification is needed—yet still require the same technical documentation standards as they would for international vendors. In short: proximity can help coordination, but it does not replace evidence-based verification of 2307m specifications.
There are several localized considerations that can affect risk and cost:
- Communication latency: Local suppliers can respond faster to clarification requests about revision or acceptance criteria.
- Shipping and return: Near suppliers can reduce time to return nonconforming items, lowering downtime.
- Stock and substitution behavior: Local distributors may carry mixed inventory. If inventory is not controlled to the same revision level, you may receive an older or different variant that shares a similar label.
- Language and documentation accuracy: Local suppliers might provide documentation in a familiar format; however, formatting clarity does not guarantee technical correctness.
Therefore, a localized mindset should apply to process speed, not to verification standards. The evidence criteria remain the same.
One helpful practice is to specify “documentation must match revision X for 2307m.” This reduces ambiguity regardless of where the supplier is located. Localization speeds up logistics, but your purchase order and acceptance plan should still enforce identity, revision alignment, and traceability requirements.
8) Comparison Table (Rephrased Additional Information)
Because no additional important information (beyond the keywords) was supplied in your request, the following table is presented as a practical, general comparison framework for handling identifiers like 2307m—focused on evidence and procurement discipline.
| Decision Area | What to Compare | What Good Looks Like for “2307m” |
|---|---|---|
| Specification Basis | Linked drawings/datasheets and revision level | Documentation explicitly ties 2307m to measurable tolerances |
| Verification Evidence | Inspection method, test protocol, acceptance criteria | Reports or statements reference the relevant testing approach |
| Traceability | Batch/lot/serial traceability | Shipping paperwork and lot codes align with quality records |
| Compatibility | Interface and integration requirements | Supplier confirms compatibility with your system requirements |
| Commercial Alignment | Lead time, return terms, documentation package included | Commercial terms match the documentation and deliverables |
9) Step-by-Step Guide: How to Procure “2307m” Safely
Below is a practical process you can follow internally when sourcing items labeled 2307m. The goal is not to slow procurement—it is to prevent expensive rework, delays, and disputes.
-
Capture the exact identifier context:
Record how 2307m appears (RFQ line item text, label photo, packing slip reference). Note any accompanying codes (revision, variant, or batch ID).
Why this matters: Sometimes the same identifier appears with different suffixes or packaging marks. Context allows you to distinguish “same label, different revision.”
-
Request the authoritative specification set:
Ask for the datasheet or drawing that explicitly references 2307m. Ensure it includes revision level, effective date, and controlled document identifiers.
If the supplier provides multiple documents (for example, one for the component and one for an assembly interface), request the full set relevant to the procurement scope.
-
Confirm measurable acceptance criteria:
Identify what is being guaranteed. Request test methods and acceptance limits rather than broad performance claims.
When possible, ask for representative test evidence for recent production batches—especially if your application is safety-critical or performance-sensitive.
-
Validate traceability requirements:
Ask how lot/serial numbers will be provided and how they will match shipping documentation.
Define what you will do if traceability is missing: will you hold shipment, reject it, or accept with a deviation? Decide before purchase so the decision is consistent.
-
Run a compatibility check against your system:
Compare interfaces, installation constraints, environmental ratings, and functional needs. Do not assume compatibility solely from the identifier.
In engineering terms, compatibility can include both “mechanical fit” and “system-level performance.” Ensure you check the items that are most likely to cause failure modes—such as sealing interfaces, connector standards, operating temperature limits, and calibration stability.
-
Normalize quote comparisons:
Compare offers using the same revision, documentation package, test evidence, and acceptance criteria. If a vendor can’t align the documentation scope, treat the quote as non-comparable.
To make this systematic, you can create a quote equivalency rubric where each missing evidence item incurs a penalty or disqualifies the quote for your application.
-
Set receiving inspection conditions:
Define what your receiving team will verify on arrival (label matches 2307m, documentation present, packaging condition, basic checks aligned with the datasheet).
Receiving inspection should include identity checks, not just count verification. If you only verify quantity, you might accept the wrong revision that happens to be physically similar.
-
Document deviations early:
If 2307m documentation or physical attributes do not match the procurement packet, stop acceptance and initiate a deviation report.
Early documentation supports corrective action and can be crucial for warranty, compliance, and future procurement decisions.
10) Conditions and Requirements (Practical Checklist)
To apply this guidance effectively, consider the following conditions/requirements. These are standard, objective procurement controls rather than industry “rules of thumb.”
- Documented link: The supplier must provide a controlled document that links 2307m to technical characteristics.
- Revision clarity: Procurement must specify revision level if applicable; otherwise, require the latest controlled revision.
- Measurable criteria: Where performance matters, acceptance must be defined in measurable terms.
- Traceability: Lot/batch identification should be provided consistently with the shipping documentation.
- Receiving verification: Your incoming inspection must include identity checks for 2307m, not just count verification.
To make the checklist operational, you can translate each condition into an action item on purchase documentation. For example:
- Add a PO line item requirement that the “certificate of conformance must reference the PO number, item number, and 2307m revision.”
- Specify that traceability must include lot number and manufacturing date, and that it must match the labeling on the physical package.
- Define an inspection step: “Verify marking and document presence; verify dimensional or functional checks per acceptance criteria.”
This turns “requirements” into “enforceable terms,” which reduces disputes because both sides know what compliance means.
11) FAQs
Q1: What does “2307m” usually represent?
2307m often functions as a technical identifier—such as a part number, model variant, or reference code. The only reliable way to know its exact meaning is to map it to the supplier’s controlled datasheet or drawing and the acceptance criteria relevant to your application.
In some organizations, 2307m might be an internal manufacturing code that is later repackaged into an external catalog. In other organizations, it might represent a calibration or measurement configuration. Both scenarios reinforce the need to validate against controlled documents.
Q2: Can I rely on “2307m” alone to ensure compatibility?
No. Even if the label matches, compatibility depends on revision level, interface characteristics, material specifications, and performance criteria. Request a documentation packet that explicitly ties 2307m to those measurable requirements.
Also consider the difference between interchangeability and compatibility. Interchangeability suggests the item can be swapped without any system-level changes. Compatibility confirms it fits and performs correctly within defined limits. The identifier might support one but not the other, depending on how it is defined in the supplier’s documentation.
Q3: How should I compare quotes for “2307m” items?
Compare like-for-like documentation scope: revision level, test evidence type, traceability details, and acceptance criteria. Unit price is secondary if the documentation and verification package differs.
If vendors do not provide adequate evidence, you should consider requesting a revised quote with the missing documentation or treat the quote as non-compliant for your application requirements.
Q4: What documentation should accompany shipments labeled “2307m”?
At minimum, ensure shipping paperwork clearly references 2307m and includes the lot/batch traceability information. For technical applications, request inspection/test statements that reflect the agreed acceptance criteria.
Depending on your risk level, you may require certificates of conformance, inspection reports with recorded measurements, and/or calibration certificates for measurement devices.
Q5: What should I do if the delivered item labeled “2307m” does not match the datasheet?
Stop acceptance, document the discrepancy (including photos of labels and the comparison between received attributes and the datasheet), and request a deviation resolution from the supplier. Early documentation helps prevent repeated failures and supports corrective action.
When you request resolution, ask for corrective and preventive action (CAPA) evidence if it is a recurring issue. Also ask whether the supplier can provide a traceable batch record that explains how the mismatch occurred.
Q6: Does sourcing “nearby” improve the reliability of “2307m” products?
Proximity can improve communication and reduce logistics delays, which may help clarification. However, supplier reliability still depends on evidence: controlled documentation, traceability, and defined acceptance criteria for 2307m.
Therefore, nearby sourcing should be viewed as a logistics and communication advantage, not a guarantee of technical correctness.
12) Expert Perspective: The Real Determinant Is Evidence Quality
From a procurement and quality standpoint, the identifier 2307m is less important than the system that verifies it. High-performing teams treat technical identifiers as part of a documentation chain. They evaluate suppliers by the strength of that chain: controlled revisions, traceability alignment, and test/inspection artifacts that correspond to measurable acceptance limits.
When organizations follow an evidence-first approach, they reduce mismatch risk, shorten troubleshooting cycles, and prevent costly downstream interruptions—particularly in applications where small differences can cause major operational impacts.
Evidence quality has several attributes:
- Completeness: Are all required documents present (datasheet/drawing, certificate of conformance, test or inspection report, traceability)?
- Correct linkage: Do the documents reference the correct 2307m revision and match the lot/batch shipped?
- Method transparency: Are test methods specified enough for your team to interpret the results?
- Consistency: Do shipping paperwork, labeling, and certificates agree?
- Auditability: Can the supplier re-produce the evidence if questioned later?
In contrast, low-quality evidence can look superficially acceptable. A supplier might provide a certificate but omit the specific test method or acceptance criteria, or provide documents that do not clearly tie to the shipped lot. These problems often become visible only after a discrepancy occurs, when time is already expensive and operational constraints are tight.
Experts also recognize that the cost of verification labor can be reduced when suppliers provide strong evidence in the first place. When the procurement packet is complete and consistent, internal quality review becomes faster and more confident. That reduces both time-to-procure and time-to-approve.
13) Conclusion: Use “2307m” as a Verification Anchor, Not a Guess
In summary, 2307m should be handled as a technical anchor that must be validated through authoritative documentation, revision control, traceability records, and measurable acceptance criteria. Whether you source from a supplier “nearby” or from farther markets, the objective standard remains the same: verify the identifier’s meaning in controlled materials and confirm compatibility with your application requirements.
If you apply the steps and checklists above, you convert 2307m from a potentially ambiguous code into a reliably governed procurement item—one that your engineering and quality teams can verify, your operations teams can install confidently, and your organization can audit successfully.
Finally, treat every successful procurement of 2307m as an opportunity to strengthen your internal system: keep templates for RFQs and evidence packets, record supplier response quality, and maintain a historical log of which documentation packages correspond to which outcomes. Over time, that institutional memory reduces future risk and makes procurement decisions faster and more defensible.
Reference Notes (for Method and Standards Context)
For general industry practices related to quality management and traceability concepts, readers may consult broadly recognized frameworks such as ISO 9001 (quality management systems) and traceability-related guidance commonly used in manufacturing quality programs. For procurement due diligence practices, organizations often align with standard quality auditing methods and documented receiving inspection controls. (No specific numeric performance claims were used in this article.)
-
1

A Guide to Cost-Efficient Small Electric Cars for Seniors
-
2
Mastering Debt Consolidation: Boost Your Credit Score and Manage Interest Rates
-
3
Your Guide to Loans, Credit Checks, and Interest Rates
-
4
Affordable Independent Living: Finding the Right Senior Housing
-
5
Guide to Senior Living Apartments: Affordable and Comfortable Environments